A planning resource for brand and sourcing teams. Engineering recommendations are not a statement of a particular project's specification, inspection standard, price, MOQ or delivery commitment.
Start with the delivered kit, not an isolated 3D model
A production file needs a definition of what the buyer will receive: runner-mounted parts, loose parts, decals or decorated components, instructions, accessories and retail packaging. It also needs an assembly target. A glue-assembled sculpture, a press-fit kit and an articulated product create different interfaces and tool risks.
Record which surfaces are visually critical, which seams can be exposed, which parts share a molded color and where the builder can safely cut a gate. These product decisions give the tool designer constraints rather than asking the tool to solve an undefined experience.
Part breakdown is a product and tooling decision
Split parts to preserve the intended form while allowing practical mold release and assembly. A split may hide a seam along an existing edge, but it can also create a fragile feature or a difficult build step. A part that looks simple from the outside may contain an undercut, deep rib or trapped geometry that needs a new draw direction, shutoff, slide, lifter or redesign.
DFM should identify these conditions before the product team treats the breakdown as final. It should also separate aesthetic preferences from non-negotiable licensed geometry so revisions can be evaluated without silently changing the approved character or object.
Review the sprue, runner and gate as one flow system
| Element | Engineering question | Buyer-facing consequence |
|---|---|---|
| Sprue and main runner | Can the melt reach the planned branches with practical pressure and material use? | Runner size, layout and the amount of non-product plastic in the box. |
| Runner balance | Do different cavities fill in a stable way when their size and flow length differ? | Consistency across parts that must assemble together. |
| Gate location | Can the part fill and pack without placing unacceptable evidence or stress on a critical surface? | Nub visibility, trimming access and appearance after removal. |
| Part and color grouping | Which parts can share material, color, processing conditions and a workable mold layout? | Numbered runner organization and the builder's ability to find parts. |
| Ejection and handling | Where can the molded part be released and handled without damage or cosmetic marks? | Part condition before packing and during builder removal. |
Resolve release, thickness and cosmetic risk before machining
General injection-molding review covers draft, walls, ribs, bosses, radii, undercuts, parting, shutoffs, venting, cooling and ejection. Model kits add a particular concern: visible sculpted surfaces often sit close to gates, seams and fine steel features. A change that improves fill may move evidence onto a visible face; a split that improves release may interrupt the sculpt.
Mold-flow analysis can support the discussion, but simulation does not replace an agreed product priority or physical trial review. The team should record which risks are accepted, which geometry may move and who approves the change.
Use prototypes for the questions they can answer
A printed or machined prototype can help review scale, silhouette, assembly access and broad interfaces. It does not reproduce every molded resin behavior, gate condition, weld line, ejection mark or production variation. Do not approve injection behavior solely because an additive prototype assembled once.
After tooling, trial parts provide new evidence. Review formation, visible surfaces, gate condition, distortion and critical fits against the agreed criteria, then document corrections and approval before routine production.
Ask for a decision record, not a generic DFM badge
- Current part breakdown, draw direction and identified undercuts or actions.
- Critical visible surfaces, parting-line priorities and acceptable gate zones.
- Material and molded-color groups with proposed runner organization.
- Critical interfaces and dimensions that require trial-part verification.
- Known fill, distortion, ejection or handling risks and proposed responses.
- Open decisions, responsible approvers and the point at which tool machining may begin.
Related project evidence
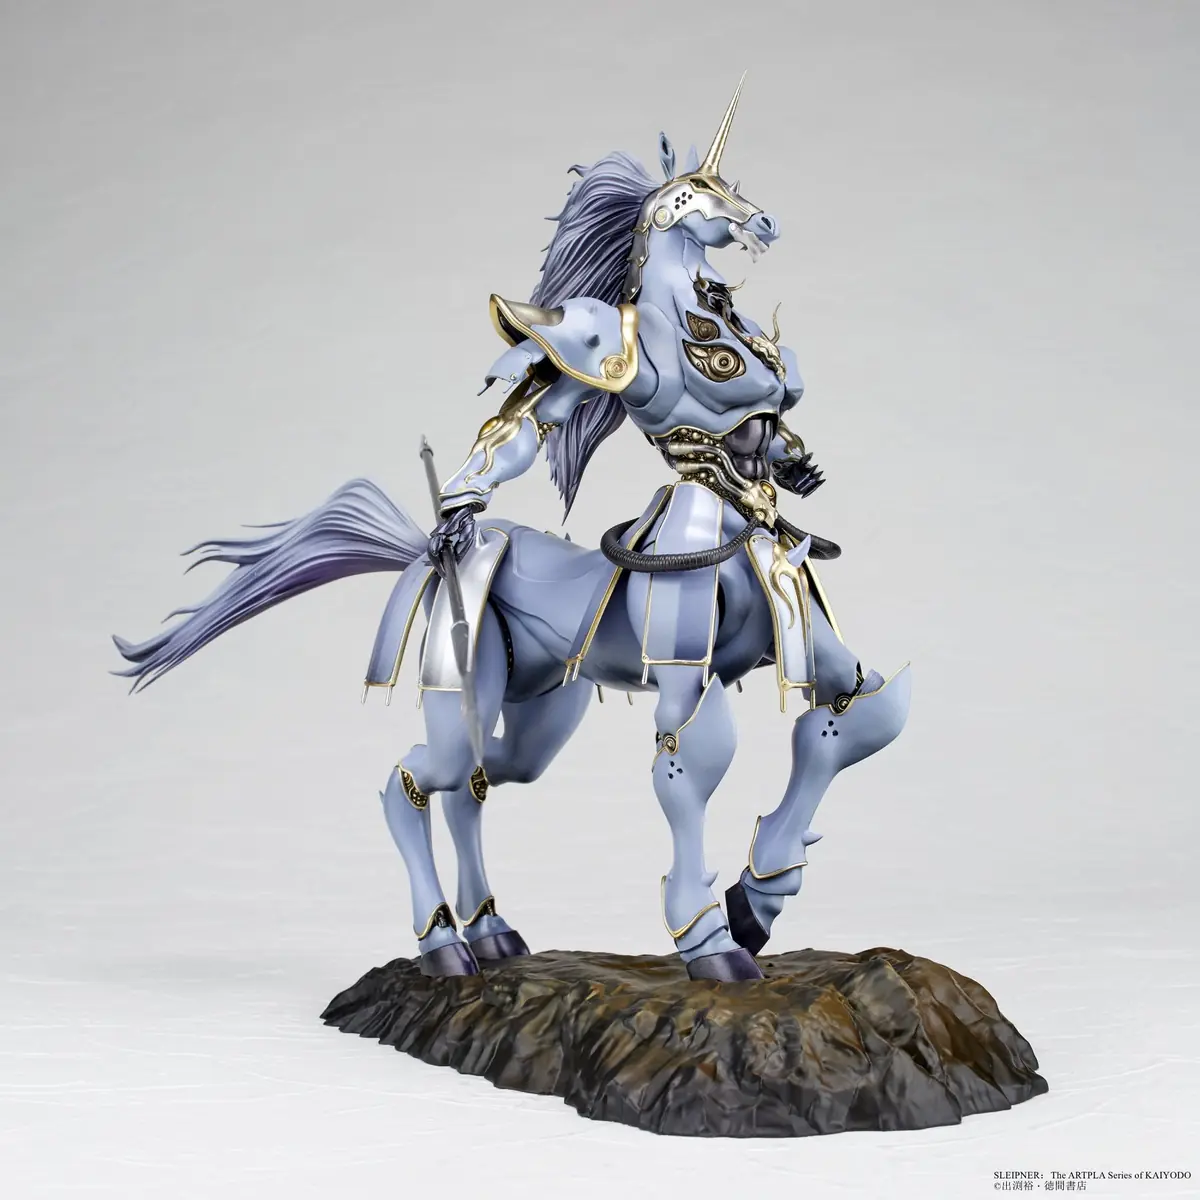
KAIYODO / ARTPLA names and images are shown with permission. The gallery illustrates the disclosed project; it is not a guarantee of specifications or test results for a new product.
Common buyer questions
Should every model kit part be placed on one runner?
No. Parts can share a runner only when material, color, size, processing and mold-balance considerations support that plan. Builder convenience matters, but it cannot replace a workable fill and tooling strategy.
Can every gate be hidden?
Not always. Gate position must support filling and packing while keeping trimming and appearance acceptable. The practical goal is an agreed gate zone and acceptable evidence, not a universal promise that every nub will be invisible.
When should the part breakdown be frozen?
It should be stable only after product, assembly and DFM questions are sufficiently resolved for tool design. Later changes may still be possible, but cost, schedule and steel-safe limits should be assessed explicitly.
References and further reading
- Protolabs — Injection Molding Guide
Manufacturing background on draft, walls, gates, material, ejection and common molding risks; not an ITTAK specification.
- RTP Company — Runner Design
Material-company guidance defining how runner systems carry melt from the sprue toward the gates and parts.
- Syuto — Plastic Model Planning, Design and Manufacture
Primary model-kit manufacturer evidence connecting CAD, mold design, machining, hand adjustment and test molding.
Plan your next step
Start with a non-confidential overview. Ask about an NDA and an appropriate transfer method before sending unreleased designs.
Request a Project Review